Why consumables must sit in the monthly budget
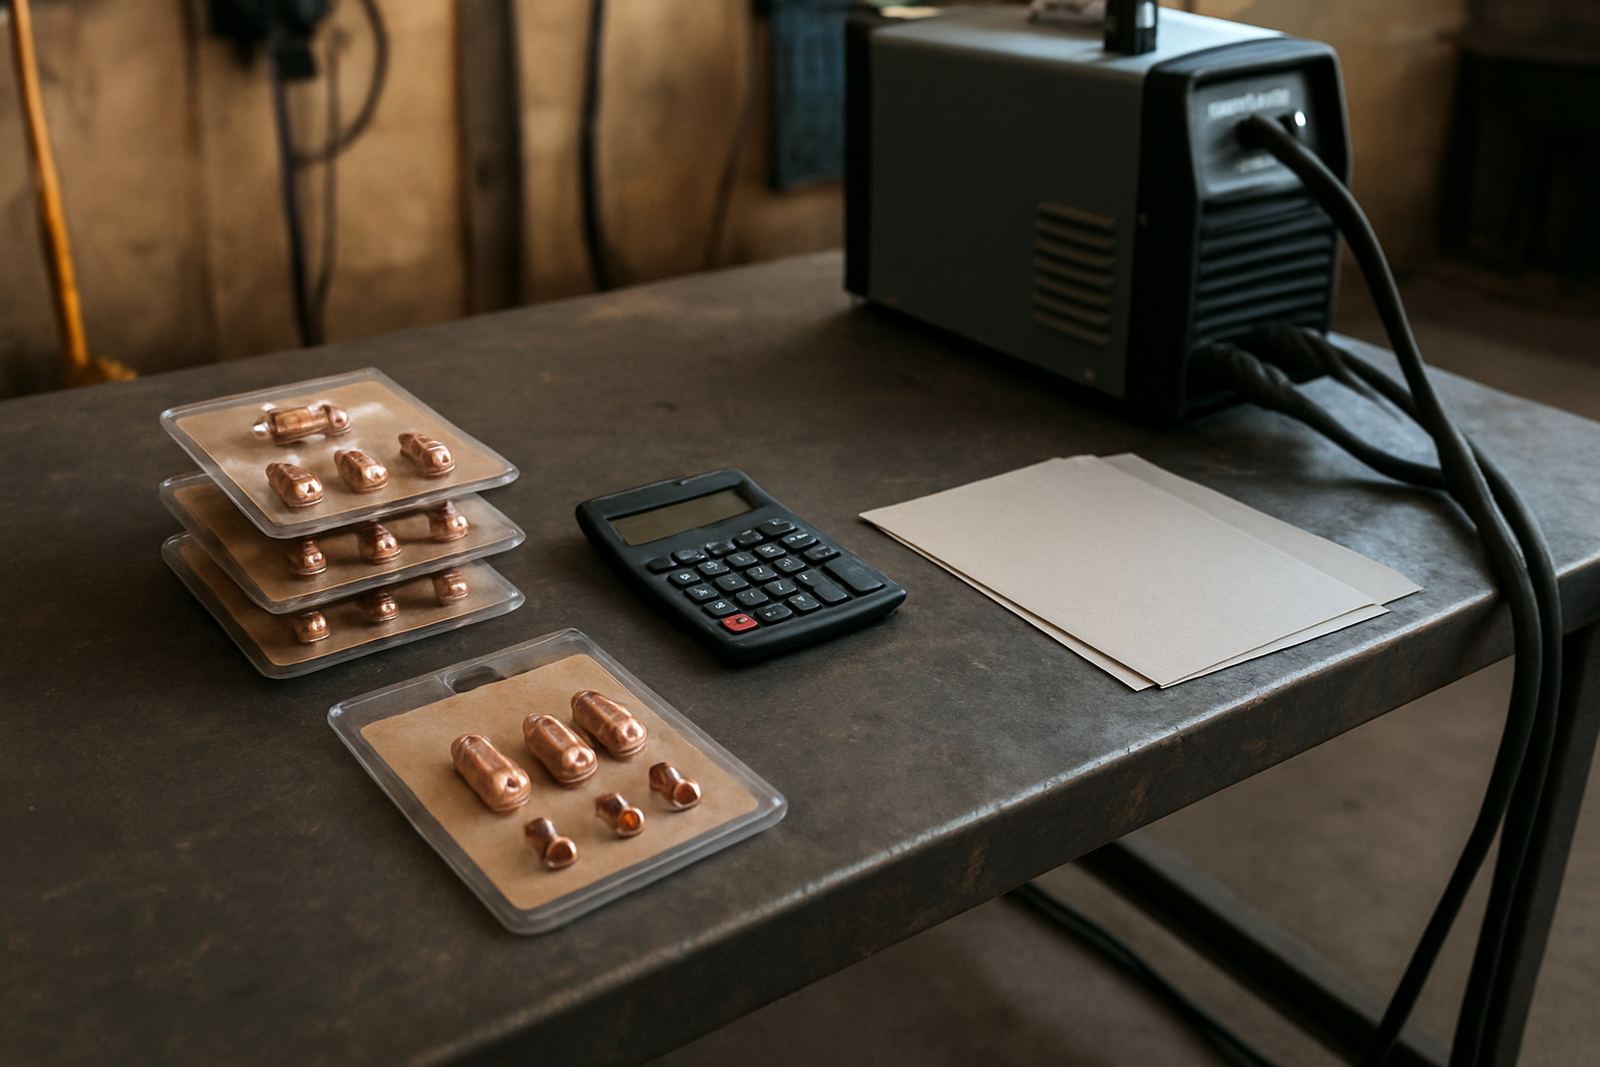
If you run a workshop in Vereeniging, Alberton or Bloemfontein, you already know that plasma cutting costs do not stop at the machine purchase. Tips, electrodes, nozzles and shields wear out with every shift, and the rate changes with amperage, steel thickness and how clean the air supply is. That means consumables should be treated like welding wire or gas bottles: part of normal operating cost, not an emergency purchase.
A simple monthly budget gives you better control over pricing and quoting. It also helps when load-shedding interrupts production, because restart work, wasted cuts and poor arc starts can push consumable use higher than expected. If you know your average use per week, you can plan stock before month end and avoid paying extra for fast replacements.
Build your budget from actual cut hours and thickness
The easiest way to budget is to track machine hours, not just the number of jobs. A cutter running 2 mm sheet all day will use consumables differently from one cutting 10 mm plate on a CNC table. Keep a simple log for each machine and note the material thickness, amperage setting and how long the torch was active.
For a small metal fabricator in Meyerton, a practical method is to calculate cost per cutting hour and then multiply by expected monthly use. For example, if your torch set normally lasts 6 to 10 cutting hours on light work, then one busy week can use up what you thought would last the month. That is why the budget must include a buffer, usually 15 to 25 percent above your average spend.
- Record cutting hours for each machine
- Separate handheld work from CNC table work
- Note material thickness and amperage used
- Add a buffer for rework, pierce-heavy jobs and downtime
Which parts wear first and how to track them
Most workshops replace the same few items over and over. The trick is to know which item is costing you money fastest and why. Poor air quality, incorrect standoff height and rough handling all shorten life. In coastal air or in a dusty industrial area, you may also see faster wear if the machine is left uncovered or the compressor is not serviced often.
- Electrodes: These carry the arc and usually show wear from arc starts and poor air quality.
- Nozzles: These affect cut shape and kerf width, so damage shows up in poor edge quality.
- Shields and retaining parts: These protect the torch and should be checked for heat damage and spatter.
- Swirl rings and insulators: Small parts, but a problem here can cause unstable cutting and wasted stock.
If you are seeing repeated failure on the same torch, it is often a sign of a bigger issue. The budget should include inspection time, not only replacement parts, because a worn air line or unstable power source can chew through consumables much faster than normal.
Local factors that push consumable use up
In Gauteng and the Free State, consumable spend can change from one site to the next. A workshop in Germiston with a dry, indoor bay will not face the same conditions as a repair crew working on site in Sasolburg dust or a farm implement job near Welkom where wind and dirt get into the setup. Even the best cutter will struggle if the air supply has water, oil or too much dust.
Load-shedding is another cost driver. When power cuts interrupt work, operators often restart jobs, re-pierce plate or cut around damaged sections. That means extra wear on tips and more scrap. If you cut on a CNC table, poor calibration or worn height control can also cause higher usage because the torch stays too close to the plate and overheats parts. A budget that ignores these local realities will always run short.
A simple stock rule for workshops and field teams
Do not wait until the last nozzle is in the drawer. Keep a basic stock level based on how fast you use parts and how long supply takes to reach you. For a Vereeniging base serving Vanderbijlpark, Sasolburg and Bloemfontein, it is sensible to hold enough consumables for routine work plus a small emergency reserve for breakdowns and commissioning jobs.
- Keep a 2 to 4 week supply of your most used parts
- Hold extra stock for high wear machines or top-up labour shifts
- Separate general workshop stock from field service stock
- Tag opened packs so old stock is used first
This keeps money from sitting in unused parts, but still gives you cover when a machine is busy for several days in a row. It also makes it easier to spot abnormal use. If one torch is consuming parts far quicker than the others, the problem is usually mechanical or air related, not just bad luck.
Turn budgeting into better cut quality and less waste
Consumable budgeting is not only about saving Rand. It is also about cutting cleaner, using less gas and avoiding rework. A well-run plasma cutter should give predictable cut quality, but only if the torch is serviced, the air system is inspected and the operator knows when parts need replacing. Training matters here because small habits like correct pierce height and clean slag removal can stretch the life of each set.
For job shops in Alberton or Bloemfontein, the smartest approach is to review spend every month and compare it with scrap, rework and downtime. If consumable spend is high but cut quality is poor, the fix may be maintenance rather than more stock. A cut quality audit can show whether the issue is in the power source, the torch setup or the way the table is being run. That turns the budget into a management tool, not just a purchasing note.